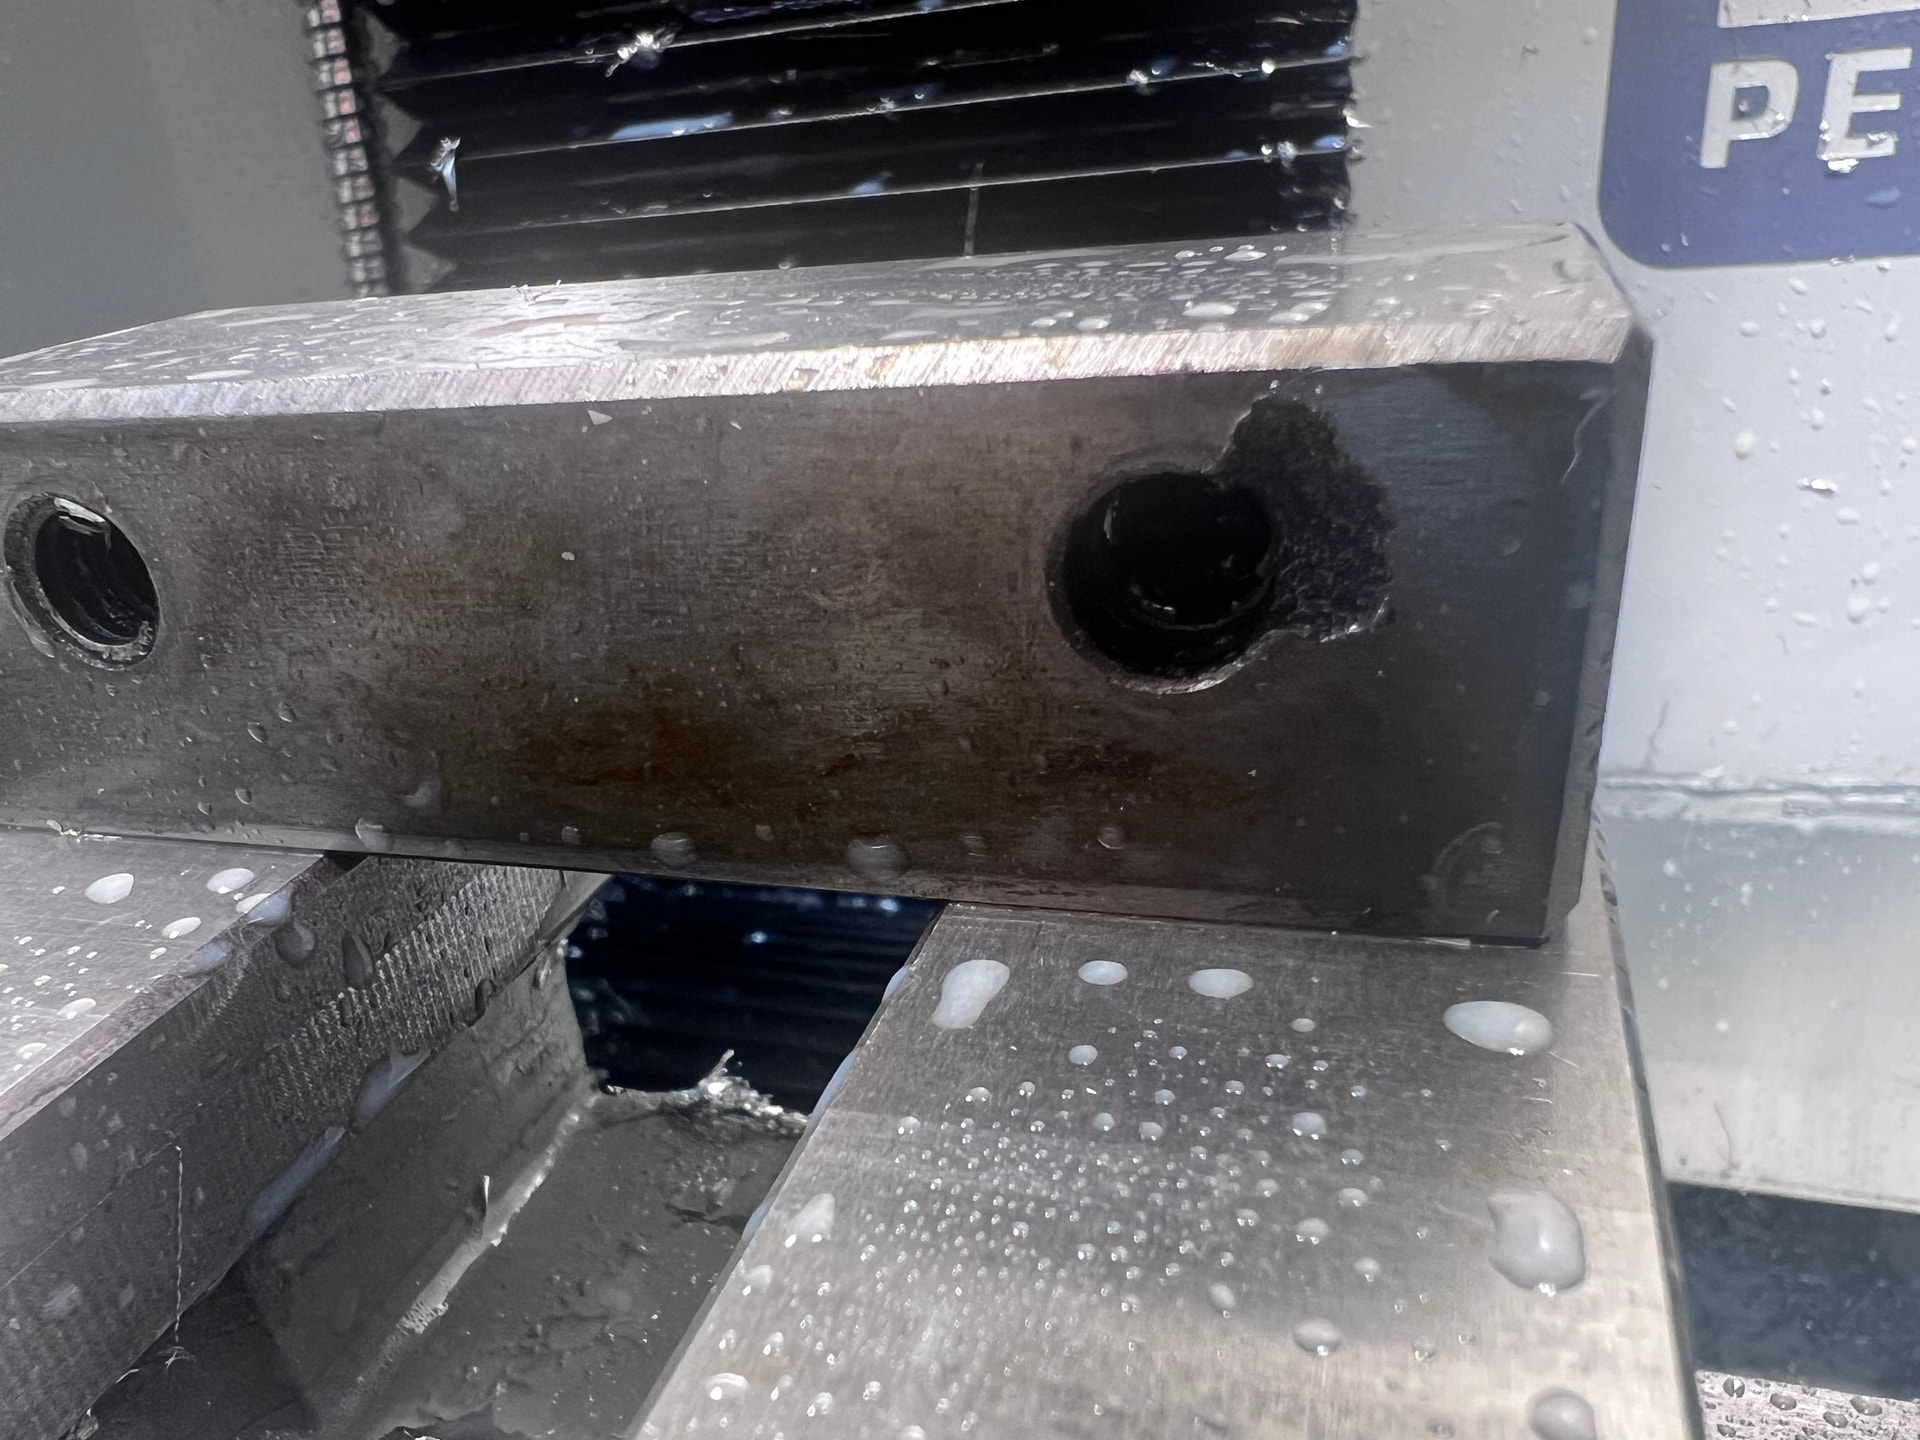
I had a part come out “wrong”. I started to check over all sorts of things until I finally made it to suspecting the thing I would have never suspected. I was checking that the Talongrip jaws were secured and parallel. I loosened them and when I started to tighten, they would not snug, so I took everything apart and found this…
Helicoil both of them. Should have clearance in the hard jaws for a maybe not so perfect locating job. Sink the helicoil 1/4 to 1/3 turn below the top. Use Red Loctite. Stone surface for high spots.
All better!
Oh, use 1 1/2 diam length helicoil.
I had looked at this and was initially discouraged of it being a viable option. Thanks for the vote of confidence and notes. I have the inserts on order and I’ll report back with results.
Step the drill size up to req’d diam if you’re doing it by hand. I’ve been told by engineers that the heli coil is actually stronger set in base material. Plus threading bolts in and out takes a toll on metals. And, clean excess red loctite out with a Q tip. Let it set for an hour or two. Otherwise the bolt will unthread it. Both locked together. No fun.
Yeah, I understand that it is a common 4” CNC vise design and the bolt spacing is standard at 2.5”. I just figured the model would match exactly and it doesn’t. The width of that part is 106mm in the model where it is 102mm IRL, so good thing I didn’t try set my WCS off the corner as I originally intended…