Food for thought…
In a very simplified example that I have training and experience in “tuning”:
A car is programmed at x injector duty cycle at the factory for certain operating conditions. The O2 sensor sees it is lean at the same conditions (because the injectors are dirty and don’t flow as much) and as such, will command more fuel to achieve the same combustion stoichiometry. End user doesn’t observe any change because there is the feedback loop. If there wasn’t an O2 sensor, then they would feel the car behave differently when it goes lean and would want to turn the dial up if they had access to it…
If a new machine tested at the factory works correctly at 5%, if a used one needs 30%, doesn’t it stand to reason that something has changed in the system where it now requires that level to provide equivalent performance and whatever that change is, needs to be investigated and remedied?
Im sure something has changed. Its a used machine. But with the table moving freely, new or used, it should hold.
There are a number of factors that could account for why im having issues. But the table moves smooth and free, it should hold. Ive talked with clearpath & tormach they are reluctant to help out other than basics. Thats why I’m messing with settings. The fine wall finish is what im trying to improve right now like I brought up in the original post. So far my 440 does better at wall finish. The 1100 holds dimensions better, but I have to run extra passes to clean the walls up and I dont think its as good as my 440.
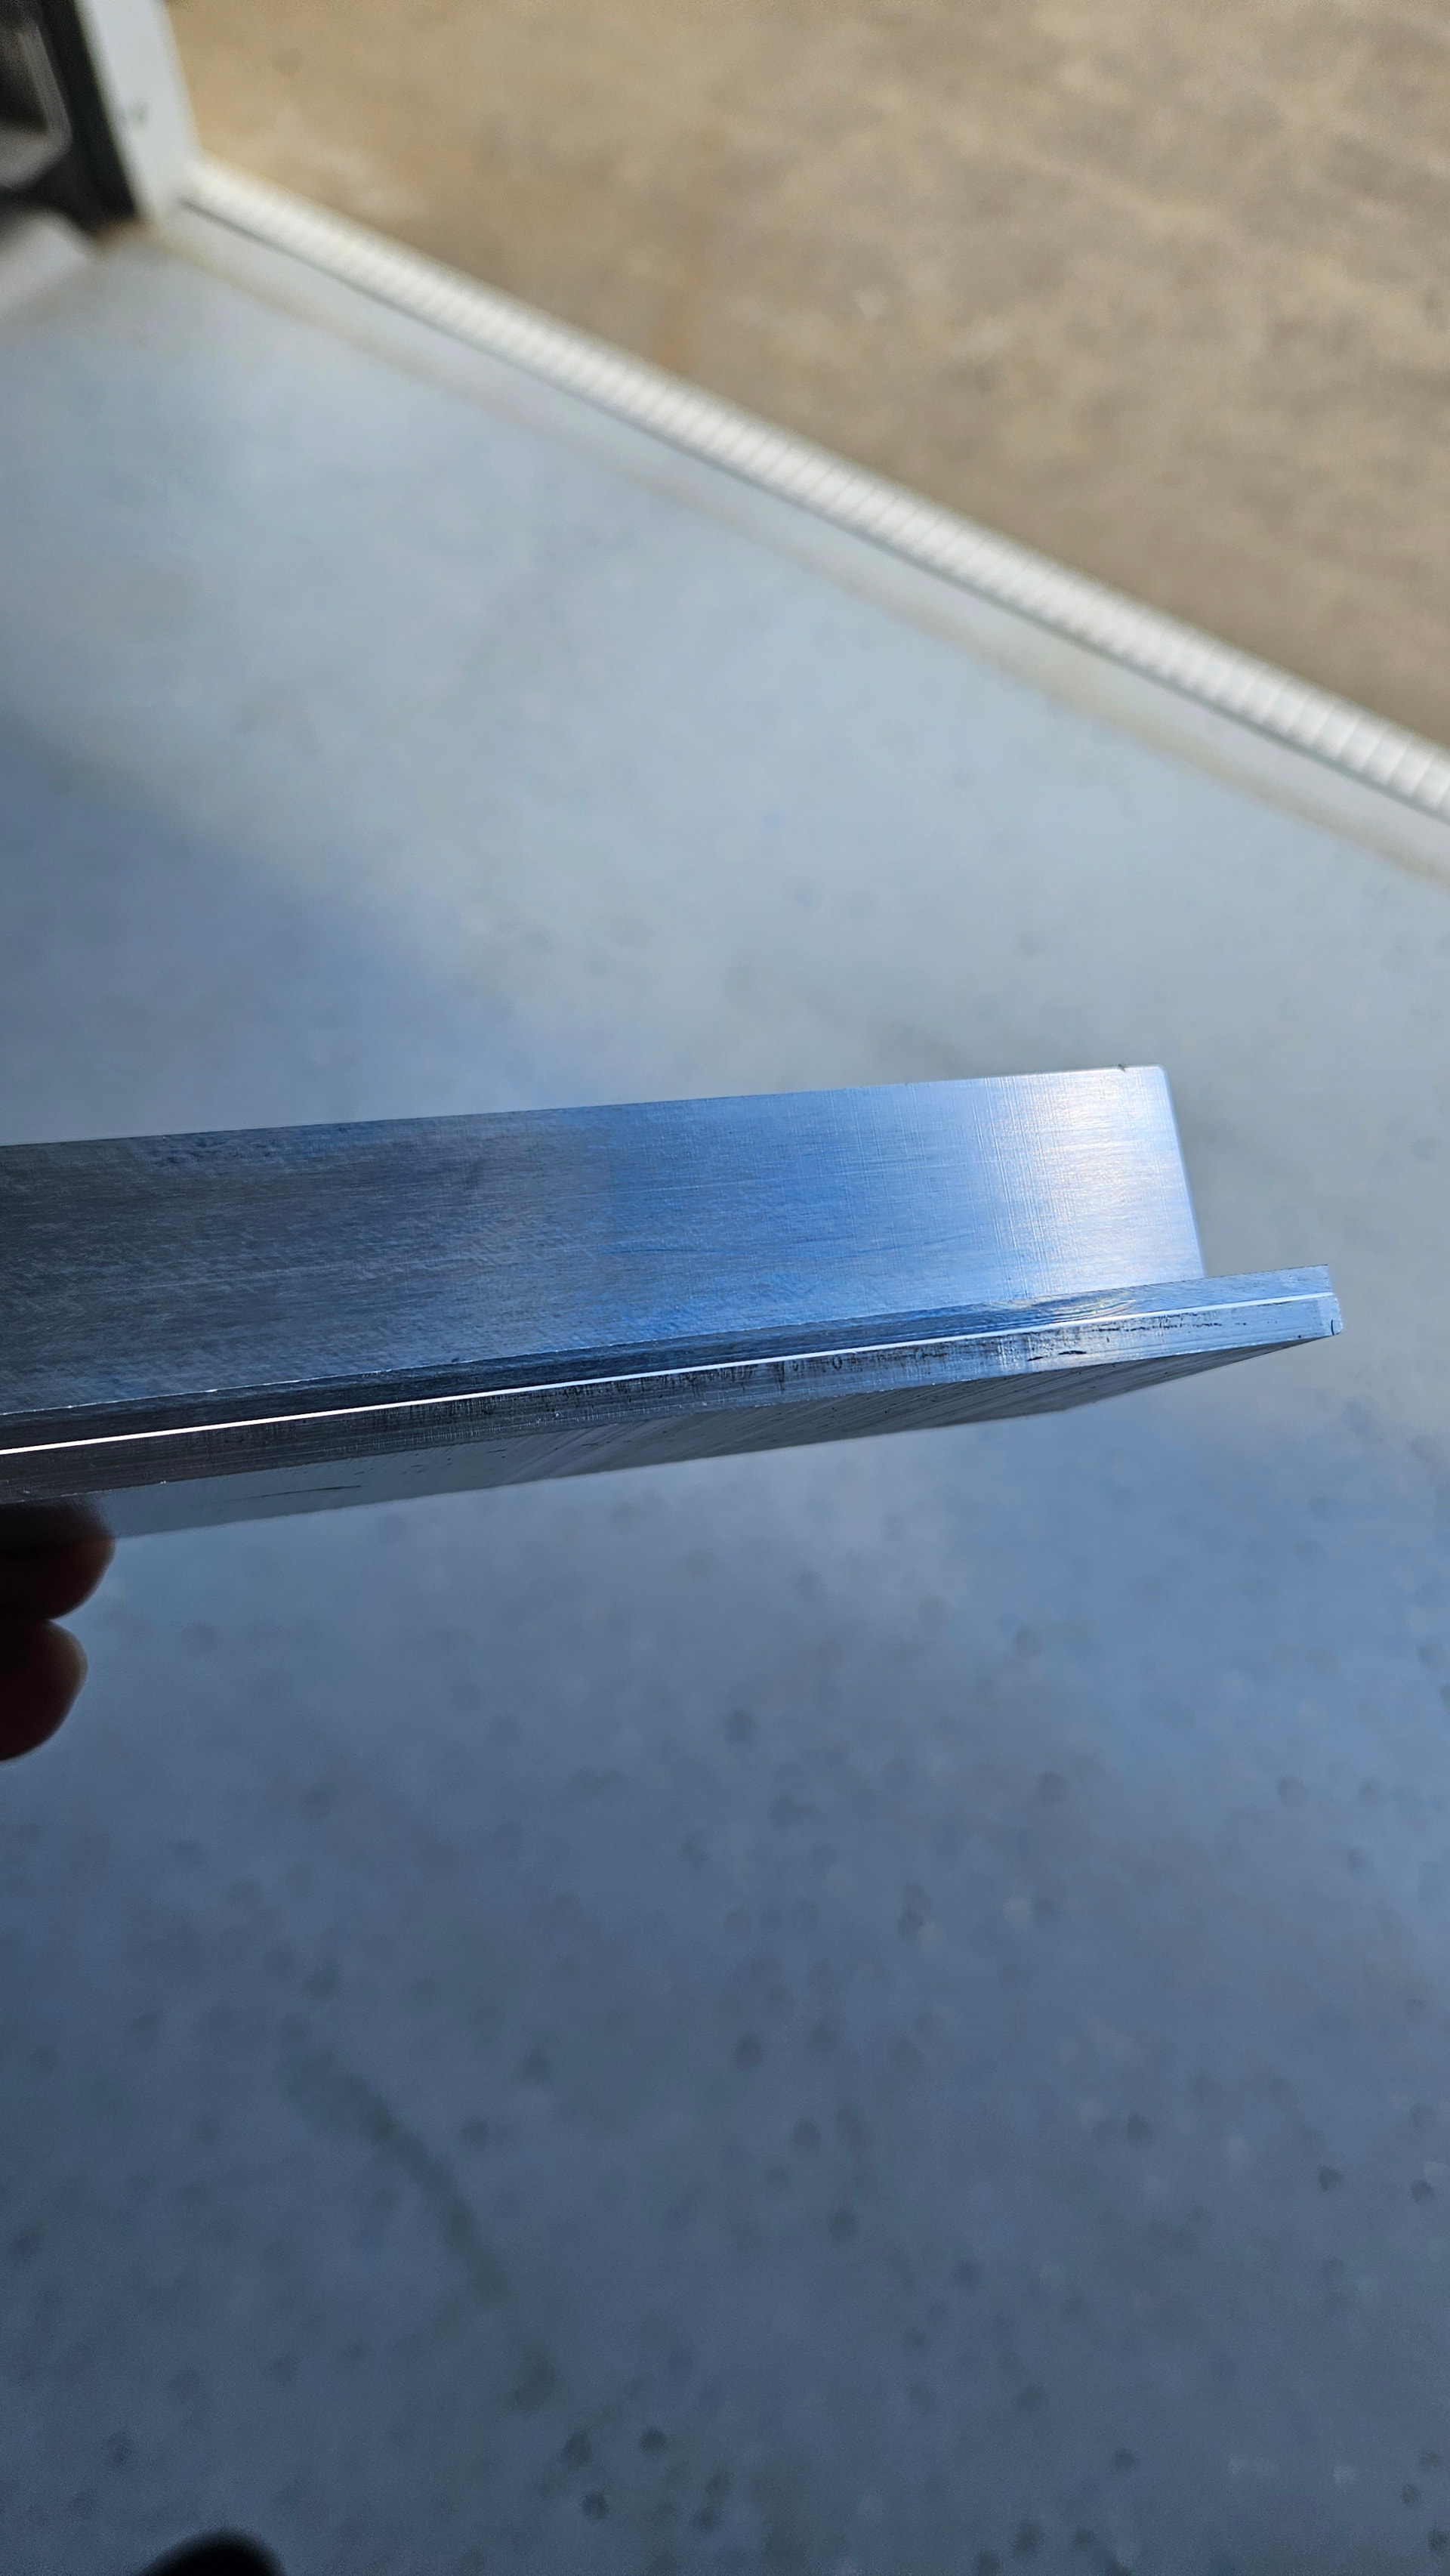
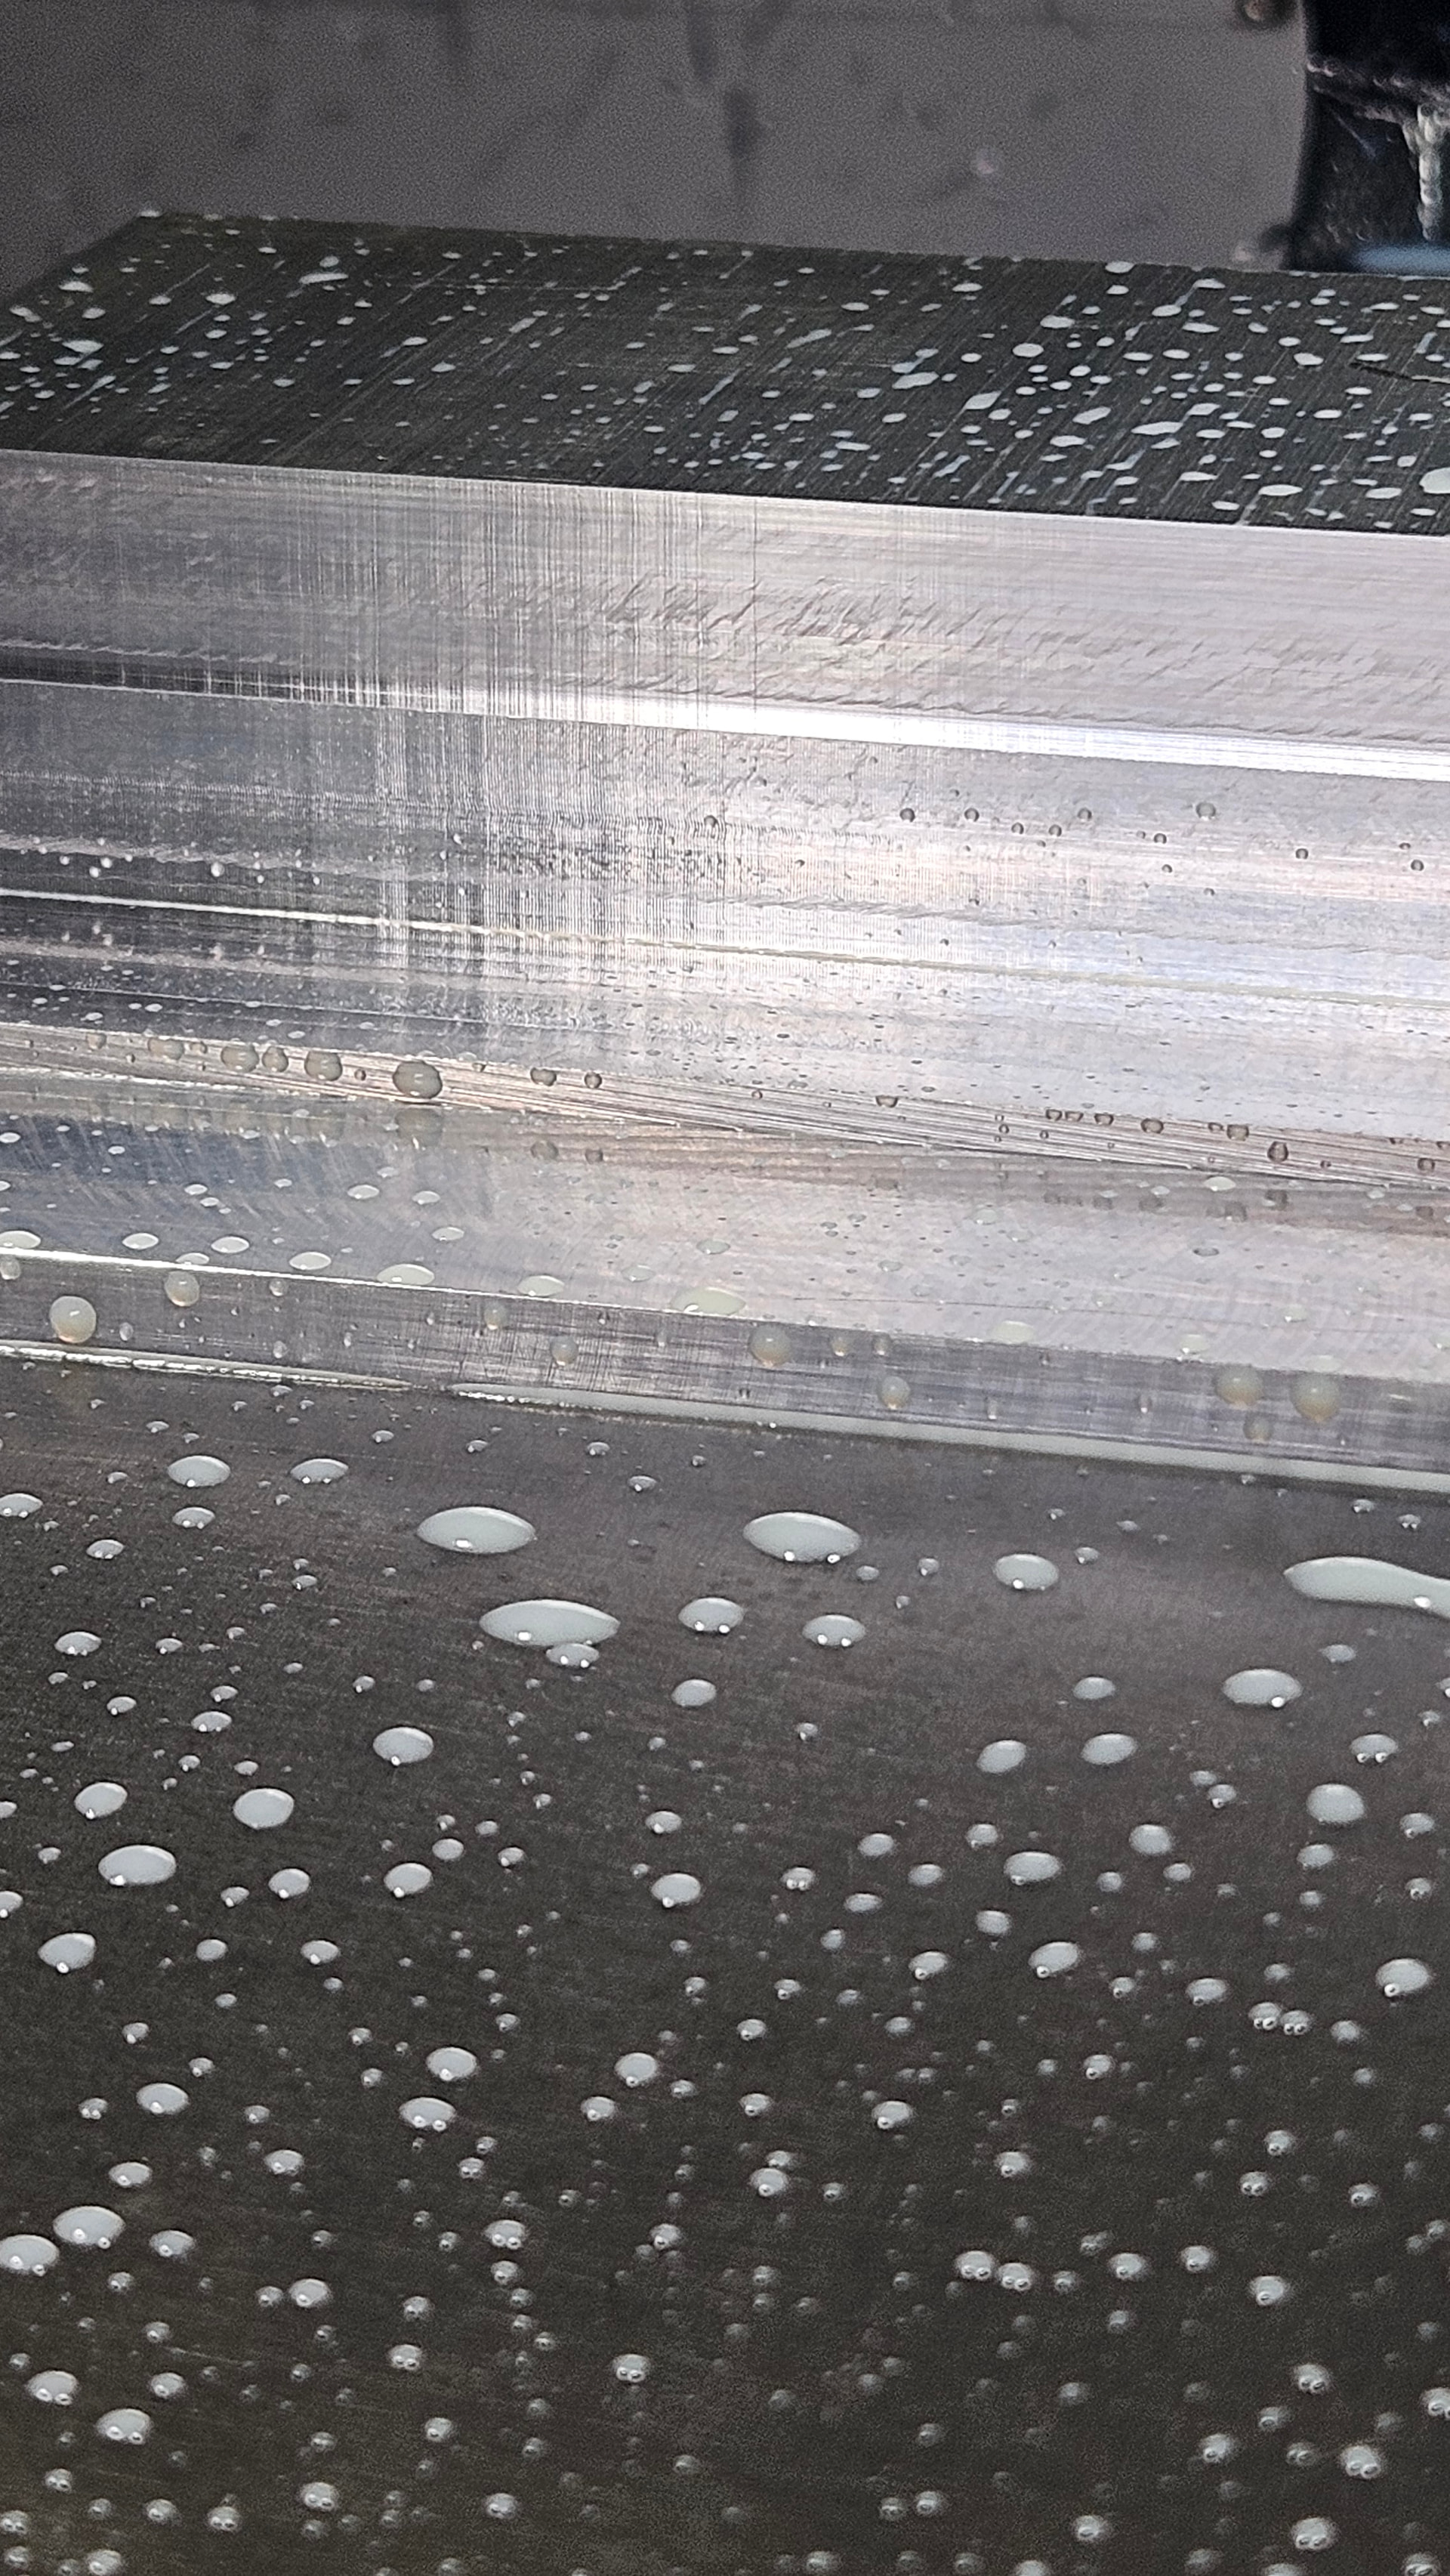
So I made some progress and I think I will let this ride for now. I need to get using the machine not working on it. I have posted some before and after. Prior to this I did go and adjust gibs 10 ways to sunday. I also replaced the AC bearings. And pulled gibs and cleaned and did a contact test.
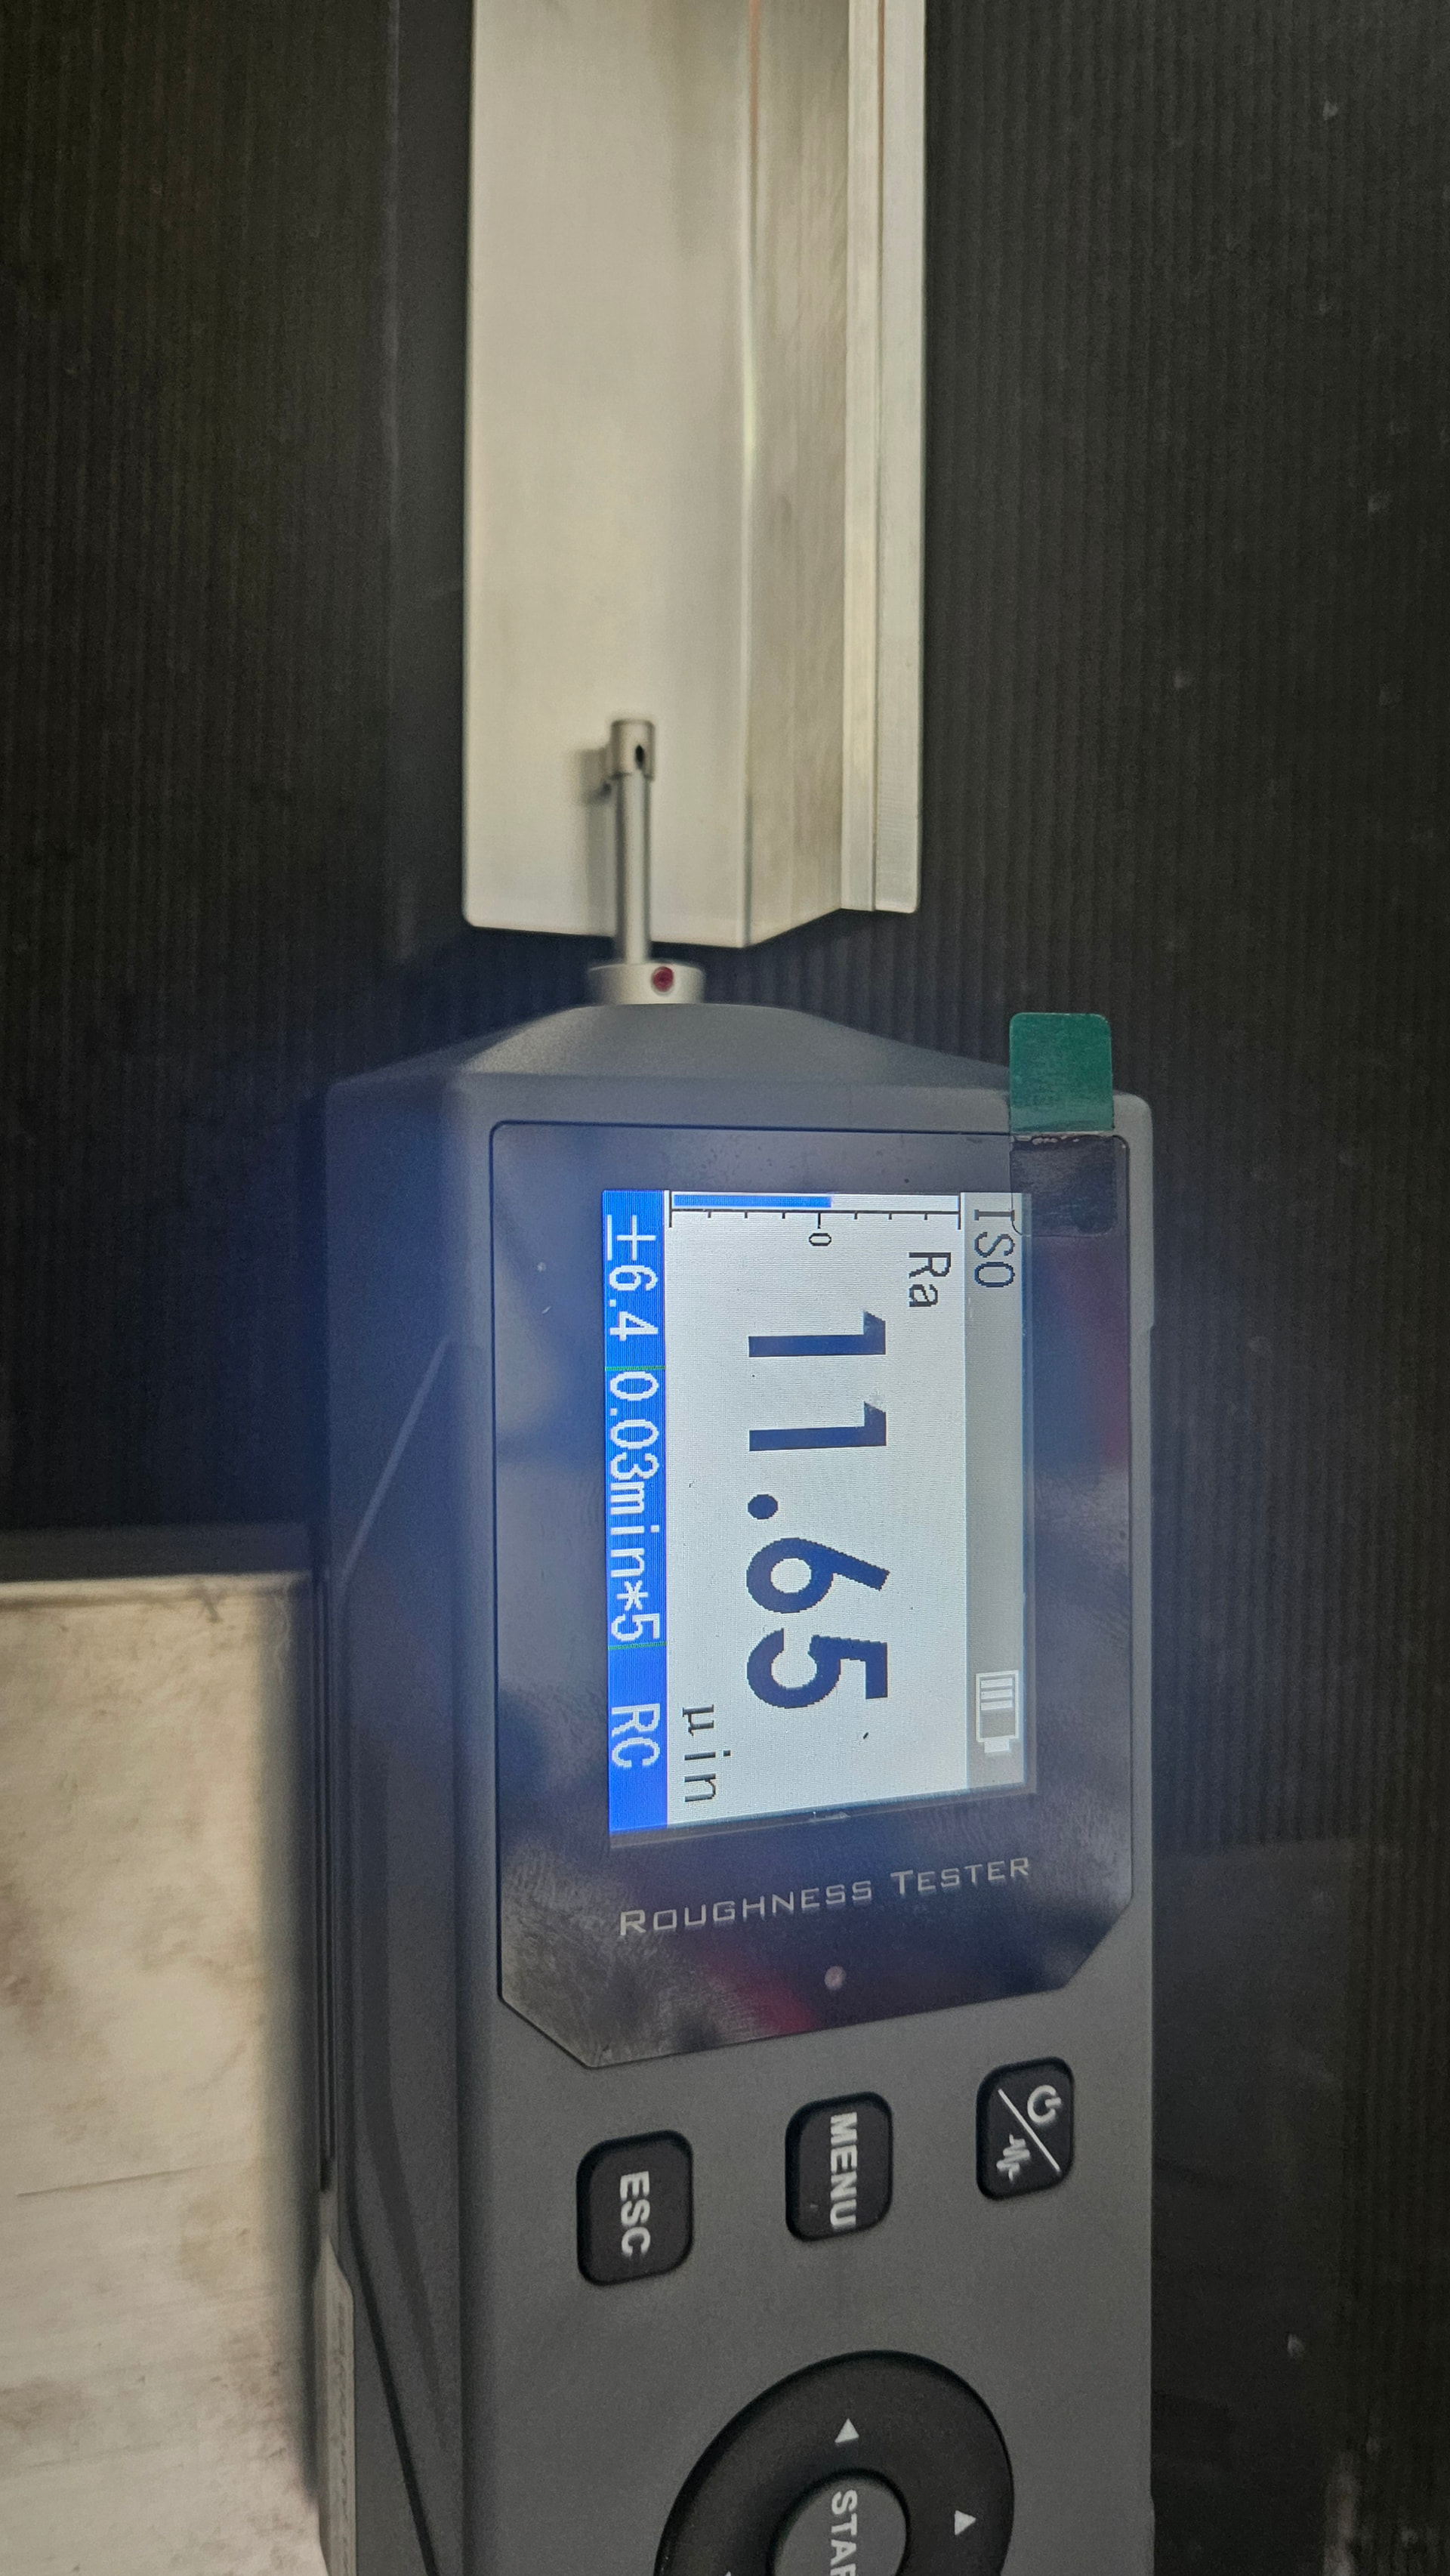
For me the solution was to do an auto tune in the servos. I figured if I dont like the auto tune, I will put in the old config files. I loaded the table with all the weight I had to put on there which was 2 - 6” vises and a dividing head. I am guessing it was between 100-125lbs. I also kept the holding torque value I mentioned in previous posts. I will do some more cut tests, but at the moment I am relieved to get this far. If you squent and angle it just right you can still see some faint lines but they are hard to see and hard to feel, even with a finger nail. When before, with a fingernail you could certainly feel them. I may be a little pickier than most, IDK. At arms length I cant see any of the lines and wouldn’t even think to look for them with the current finish. Keep in mind pictures seem to really exaggerate how bad the lines are in both the before and after pics. There can be endless debate as to why I needed to go through this and so many of you have great running machines. And I am jealous of you and hopefully after some more testing I can move on and chalk this up to used machine blues.
So if you are having similar issues as this post. And there were 2 issues in this post. The initial fine resolution lines and the big bump/thump lines which I didn’t find till after starting this post. I hope this will give others some info to go on to get to an acceptable finish. I would call this finish acceptable, I would like it to be better. Meaning I see no lines no matter how hard I try.
Word to the wise the 7202B bearings come in many flavors. I recommend you get an AC bearing with the metal cage not the plastic ones. I had issues getting SKF bearings in spec no matter how hard I tried. I then switched to nachi and setting the AC bearings took 5 min. I used the kluber? grease in them.
Angular contact bearings. There are 2 on each axis.
Sorry, which ac bearings did you replace? Spindle?
Edit
Oh, ball screw support bearings?
I disassembled the spindle, cleaned and Klubered the bearings early in the 770mx’s life. Had chatter issues too. Between new grease and gib adjustment, and table lube and cleaning, it went away.
Spindle is fine. I replaced axis ac bearings.
This isnt a chatter issue. This is a servo configuration issue. I mention the gobs & ac bearings because that the first thing everyone points to. But for me those were not the problem. Chatter can be influenced by the operator. The fine lines i show in the post happen no matter what feeds & speeds or end mill i use and the lines never vary.
I wanted to get help & give help for others who are struggling with wall finish & perhaps help people recognize when its not a chatter or usual mechanical problem.
I plan to test more & share. Tormach won’t suggest servo settings & clear path points to tormach. If the basics dont fix your problem you’re on your own. So I hope to fill in the gap they leave.
Did you look closely at the tool path? NX can do wierd things like faceted arcs depending on tolerance settings among other things. Very small deviations.
This is using tormach conversational, straight line movement.