Bought a used 1100mx, 2020 is the production year. But it seems to have some chatter on both X & Y and I can not figure out why. I am running the same feeds and speeds as my 440 which has NEVER chattered.
I have tighten gibs, angle contact bearings, checked tool runout, verified oiled ways, tried different feeds and speeds. My 440 I run 40ipm, 0.03 WOC, 0.5 DOC, 3FL 1/4 end mill and it passes the fingernail test with flying colors and no visible signs of chatter. Same settings on 1100mx doesnt pass the same tests.
Whats the trick to making this thing happy. I have heard that servo motors can be the issues, but I can thats seems crazy to me that Tormach wouldnt have good motor tuning form the factory. Id expect them to be conservative in their settings, to make sure they had nice finishes.
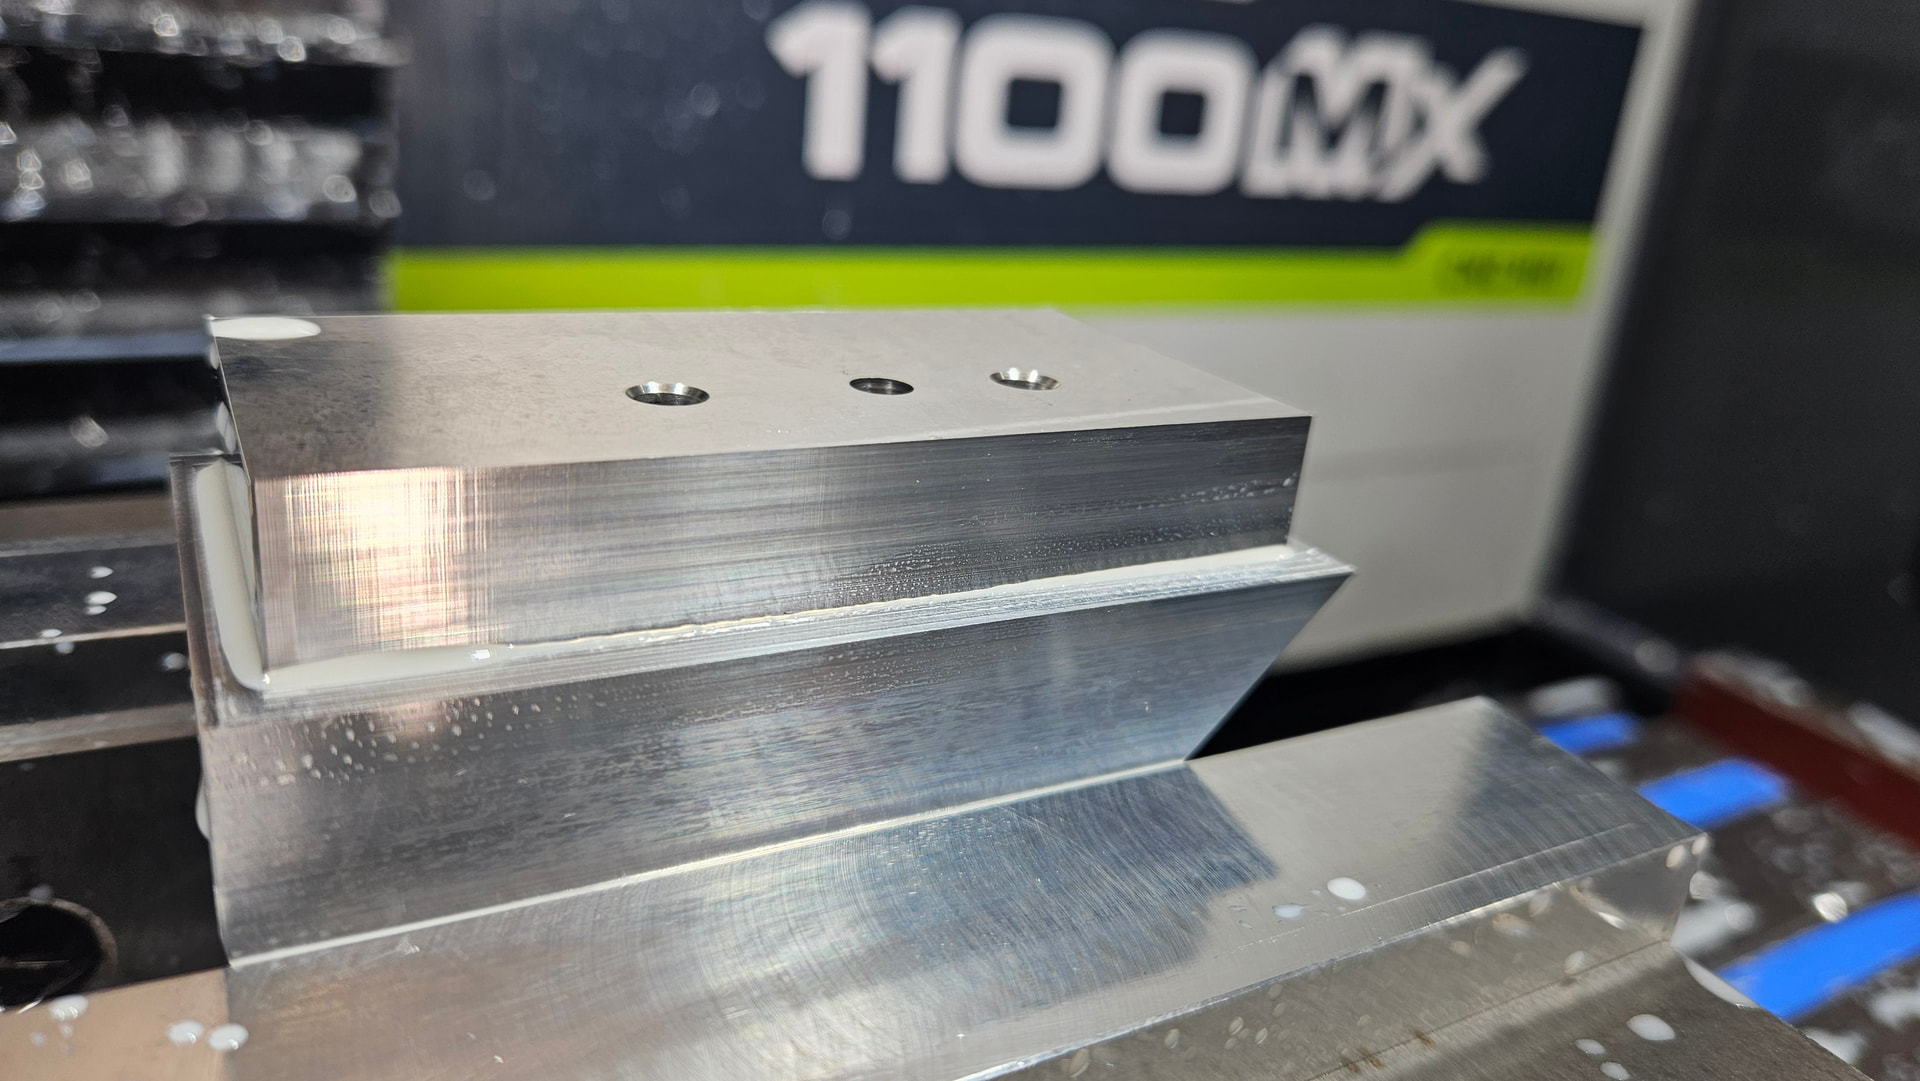
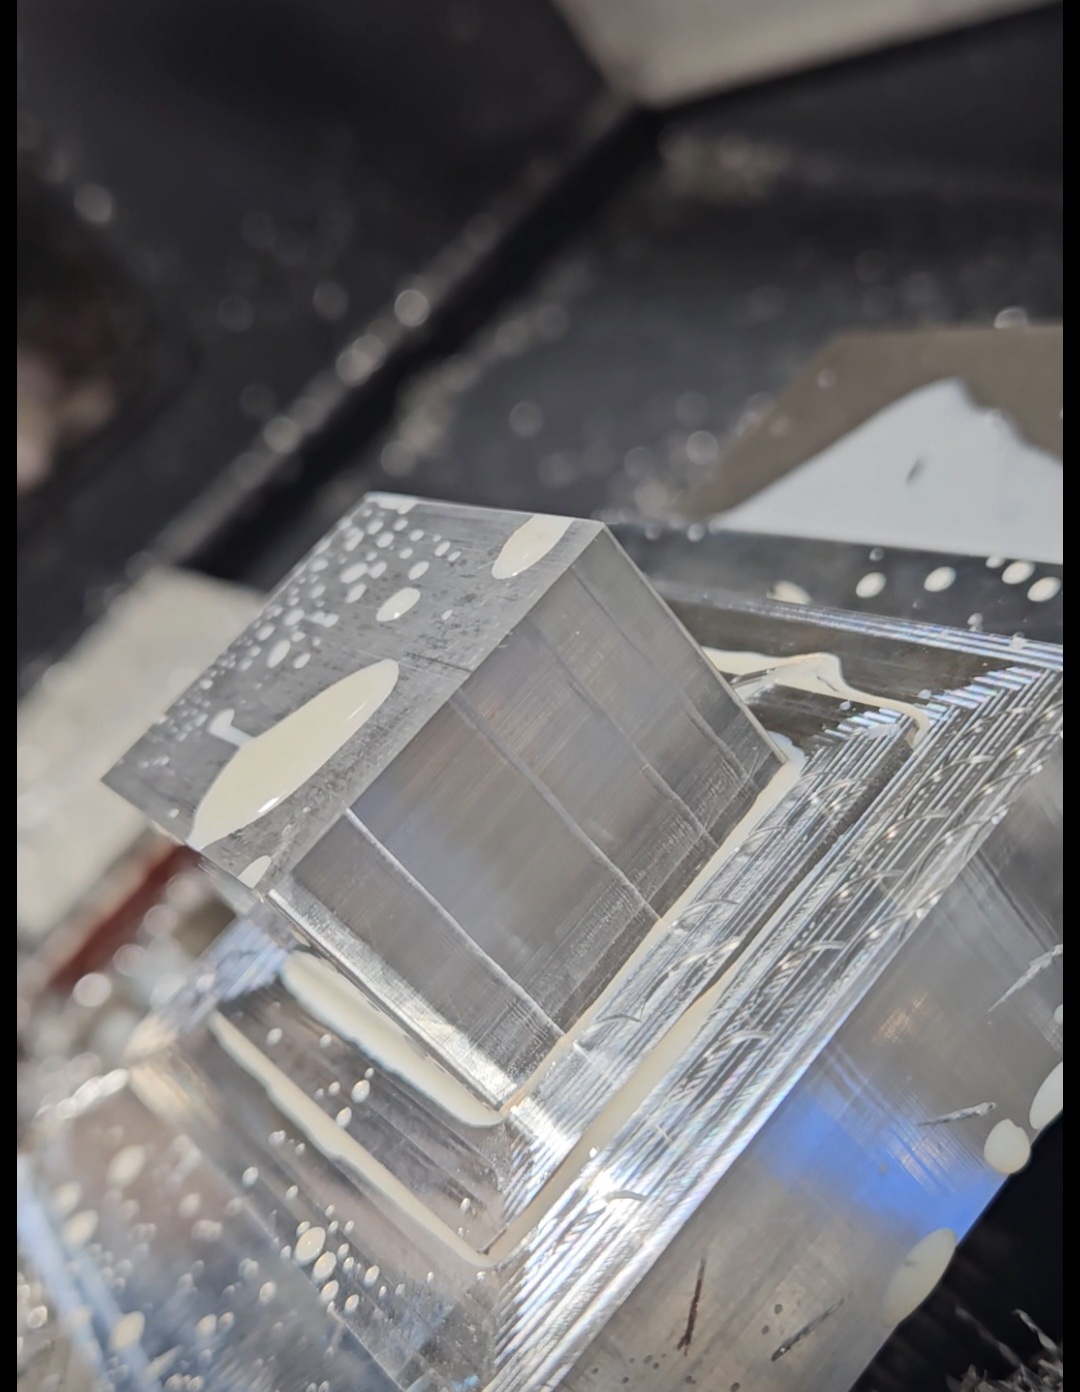
The upper 0.5 inch is the 1100mx, the lower part was from the 440. The 440 had a 3/8 end mill with 2.25 stick out and has better finish.
It is odd that the same recipe that worked on the 440 doesnt work on the 1100
FWIW…I never use 1/4” EM unless needed to mill a hole or slot… basically I use the largest EM possible up to 1/2”… so for profiling an exterior I use a 1/2” 3FL YG-1 EM … roughing at 9000 RPM 120 IPM .03 WOC up to 1.25 DOC…. Finishing cut is 40 IPM .005 WOC full depth at 9000 RPM
As long as we’re playing find the wiggle have you put a dial indicator on the spindle, my 1100mx spindle runout is super ultra low, like my .002mm dial just barely moves within error tolerance.
I’ve had occasional chatter crop up on my MX1100. Checking all the usual sources and working with the Tormach help center to track down any sources of chatter resulted in little improvement. After about a month of fruitless adjustments I finally checked the coolant concentration using a Refractometer ( I use Tormach’s recommended Xtreem Cut 251C ). It was reading below 5 brix . Readjusting it to 8 brix significantly reduced the chatter. I cut mostly stainless steels and titanium and have found clean filtered coolant with a concentration of around 10 brix provides the right balance of cooling and lubrication. Be aware that QualiChem’s recommendation for milling is 7.0 to 9.0 brix.
One more thing that most folks don’t do is check the drawbar tension. I used a Haas 30-Taper spindle drawbar force gauge (part no 09-0571) and found that the tension was about half of the specified force. New belleville washers from Tormach brought the tension up to spec, but didn’t improve the chatter. Now most folks aren’t going to fork over $300 for a gauge, so if your machine is over 5 years old just replace the washers as part of the maintenance schedule.
I need to get one of those. Do you have a part number? I need a long em for cutting the outside profile.
I have a 3/8 long 3 fl, cheapo em & the machine doesnt like it. If I take a 0.03woc, 1.1 doc, 7500rpm @40ipm the machine bumps & thumps - messes up the finish. I think the servos are fighting against tool pressure. So after looking at recommended specs, I had to slow down to 5500rpm and it was better but still get the occasional bump/thump. I have an old 3/8 tormach em and I can take a 1"doc same f&s as before & run hard till spindle bogs and the machine doesnt bump/thump. The machine just doesnt like that long cheapo em.
I just received the no-name import 4” long 3/8” 3FL with 1.75” LOC I ordered because I had nothing that could get down to that depth for a bore. I don’t have a boring bar, not sure if I should contemplate adding one to my inventory. Not sure when I’ll cross over from “still learning” to spending 2-3x more on “brand name” carbide since nothing I’m making (yet) pays for itself…
Thats what I got & my machine doesnt like it. I hope yours does. Then I know o got an issue thay needs to be fixed. My 440 can take light cuts with it or it will bog. But no funny business.
The 1100mx, it bump & thumps & messes up the finish. Let me know how you do with it.
I ordered a long 3/8 yg1 yesterday so I have something to compare it to.
Personally I think i have issues. I dont see why the cheapo shouldn’t work. I use lots of cheapo end mills and even my 440 has no problem with them.
I’ve found that el-cheapos are often highly variable one to the next. You can get a great one and swap in another just like it and it’ll be a squeal-fest at the same settings.
It’s also possible the spindle bearings got thrashed by the previous owner. I had a used 1100 like that. Swapping the spindle out was a night and day difference.
It doesnt squel. The cut seems normal, then a random bump/thump and there is a vertical gouge. But between gouges seems normal.
Spindle is quiet & I can run standard length 3/8 em at 1"doc, hard & no problem. I can run it hard enough to bog down the spindle. But run the long 3/8 at 1.1"doc and a modest cut causes issues. I dont understand the issue exactly. Im waiting on a 3/8 long yg1 em to test & see if it does the same thing.
I think its either your holder/collet or the machine itself
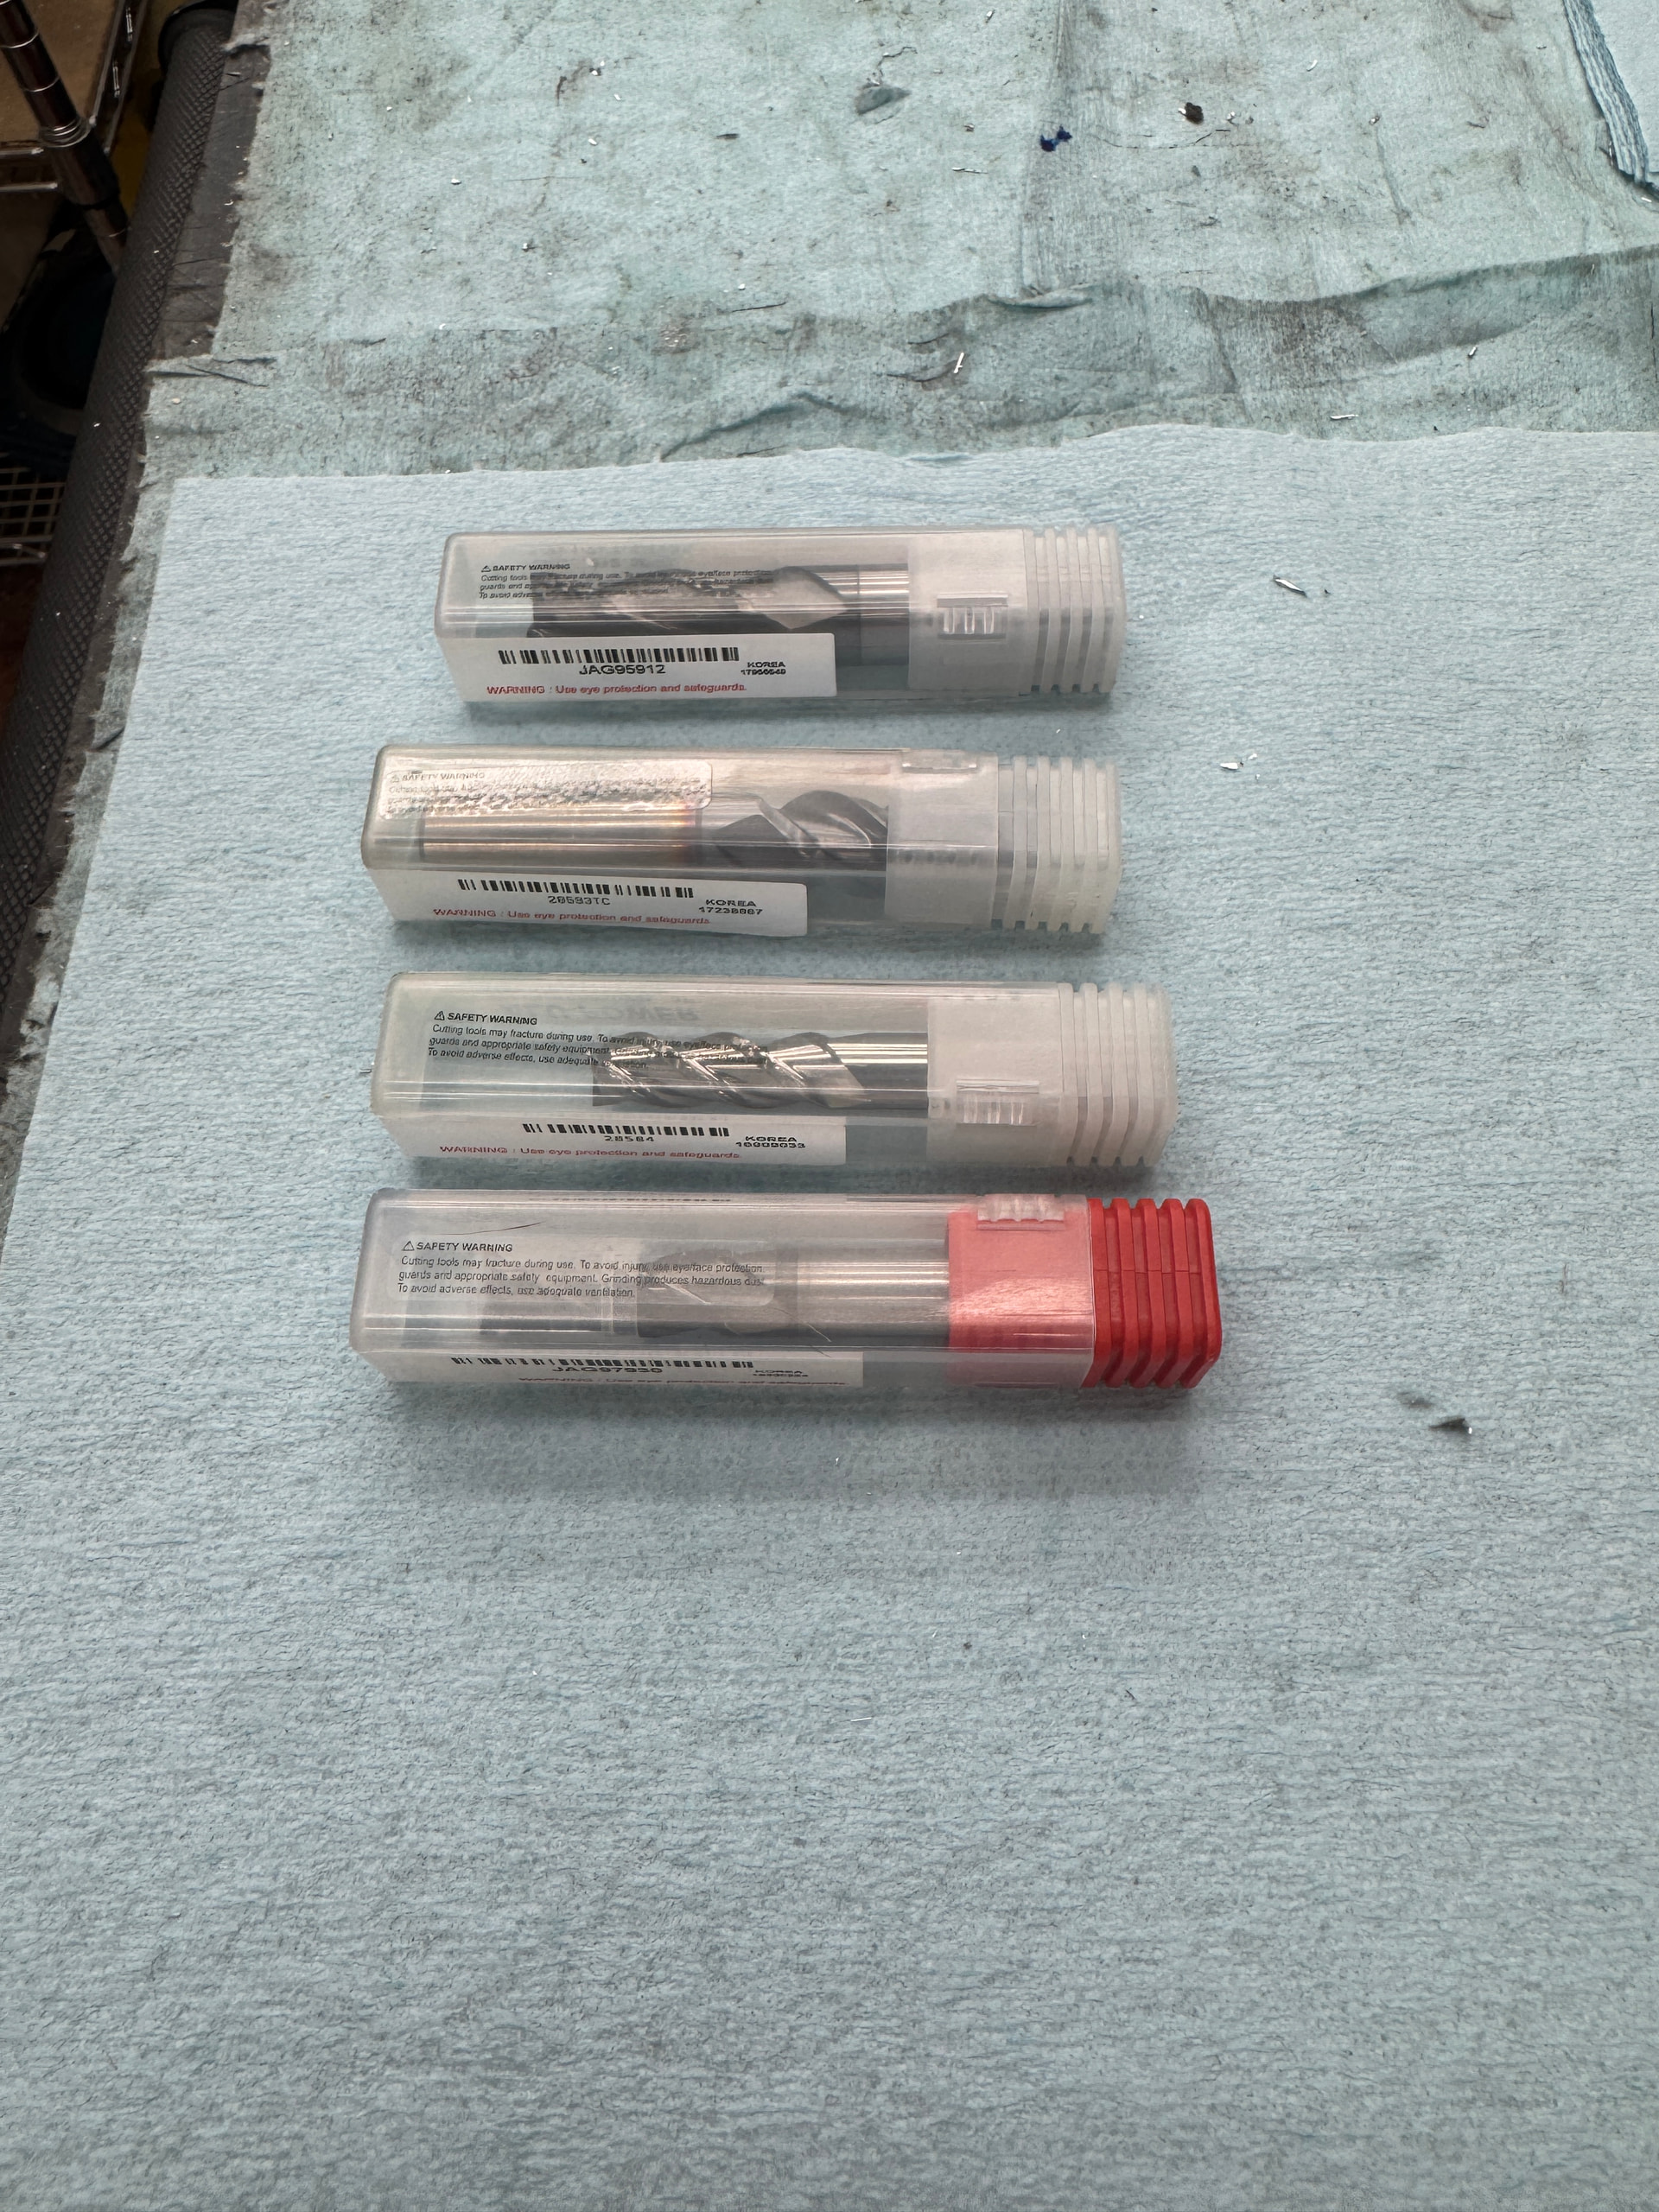
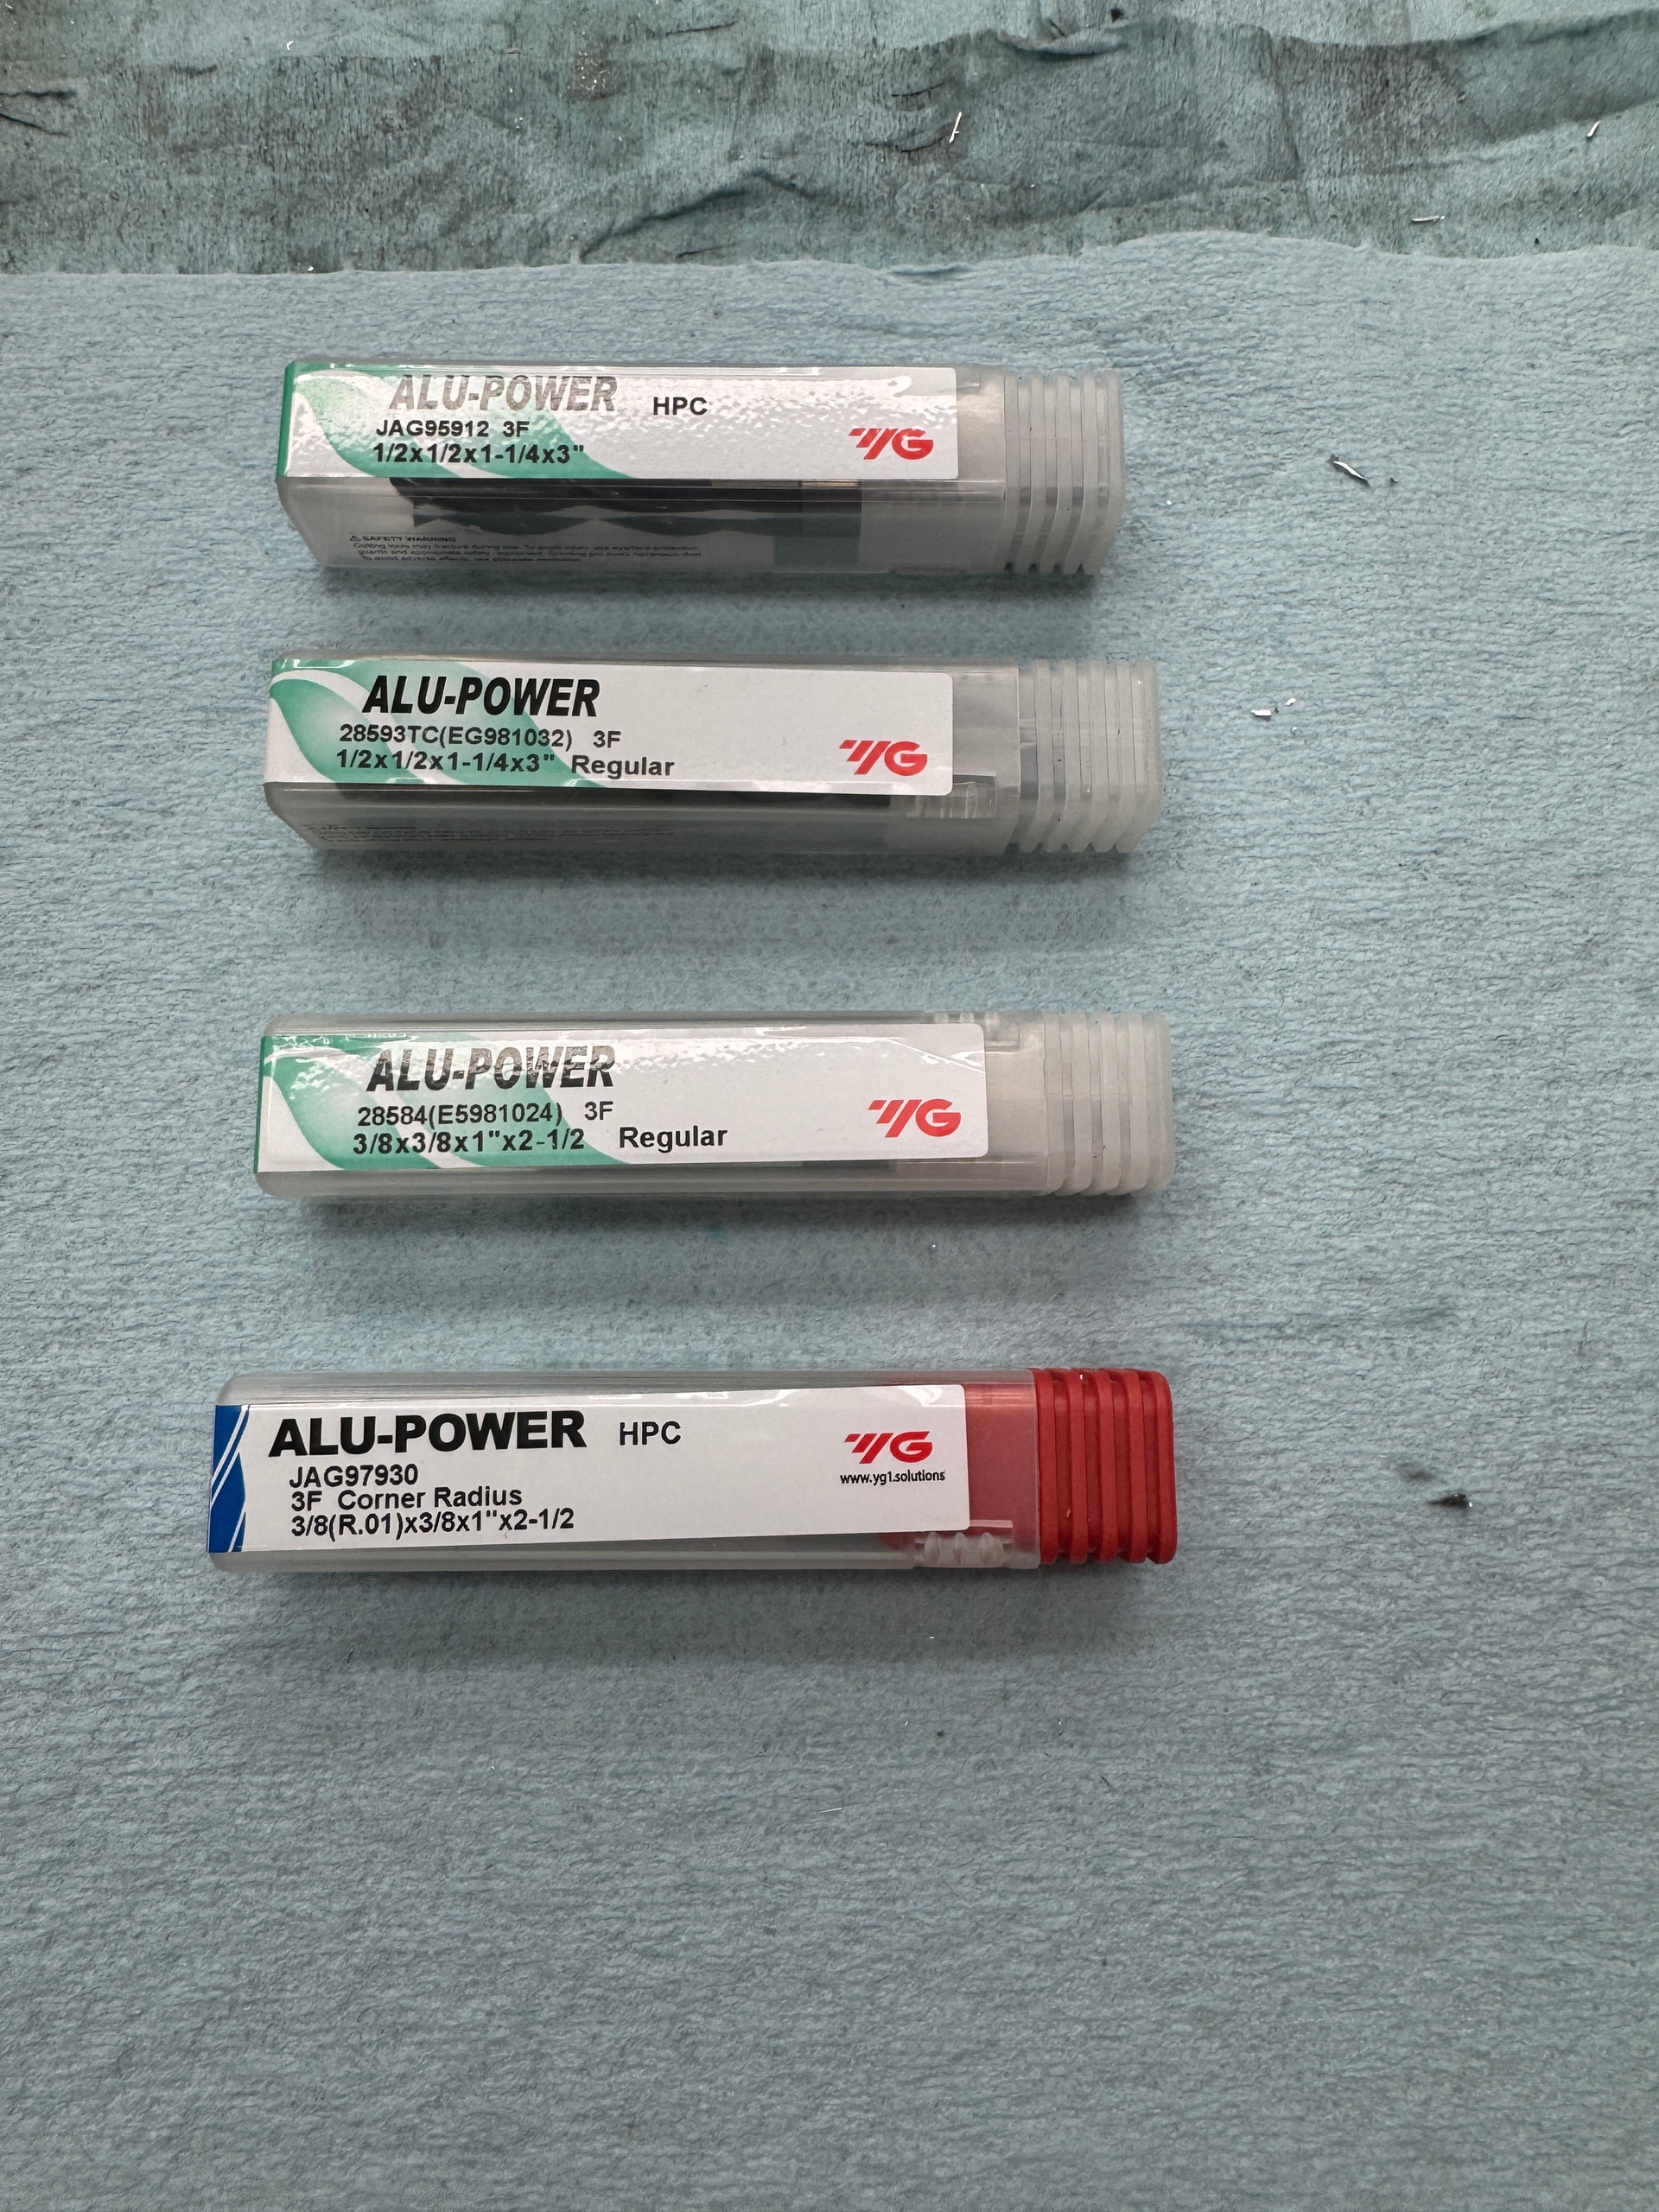
here are the 3 versions of YG EM’s I’ve used
The most expensive is the JAG… although it lasts longer with its high end coating I could not get a better finish than the TC or no coating so I use it for roughing….. the bare carbide make a great finish and I will just get those in future
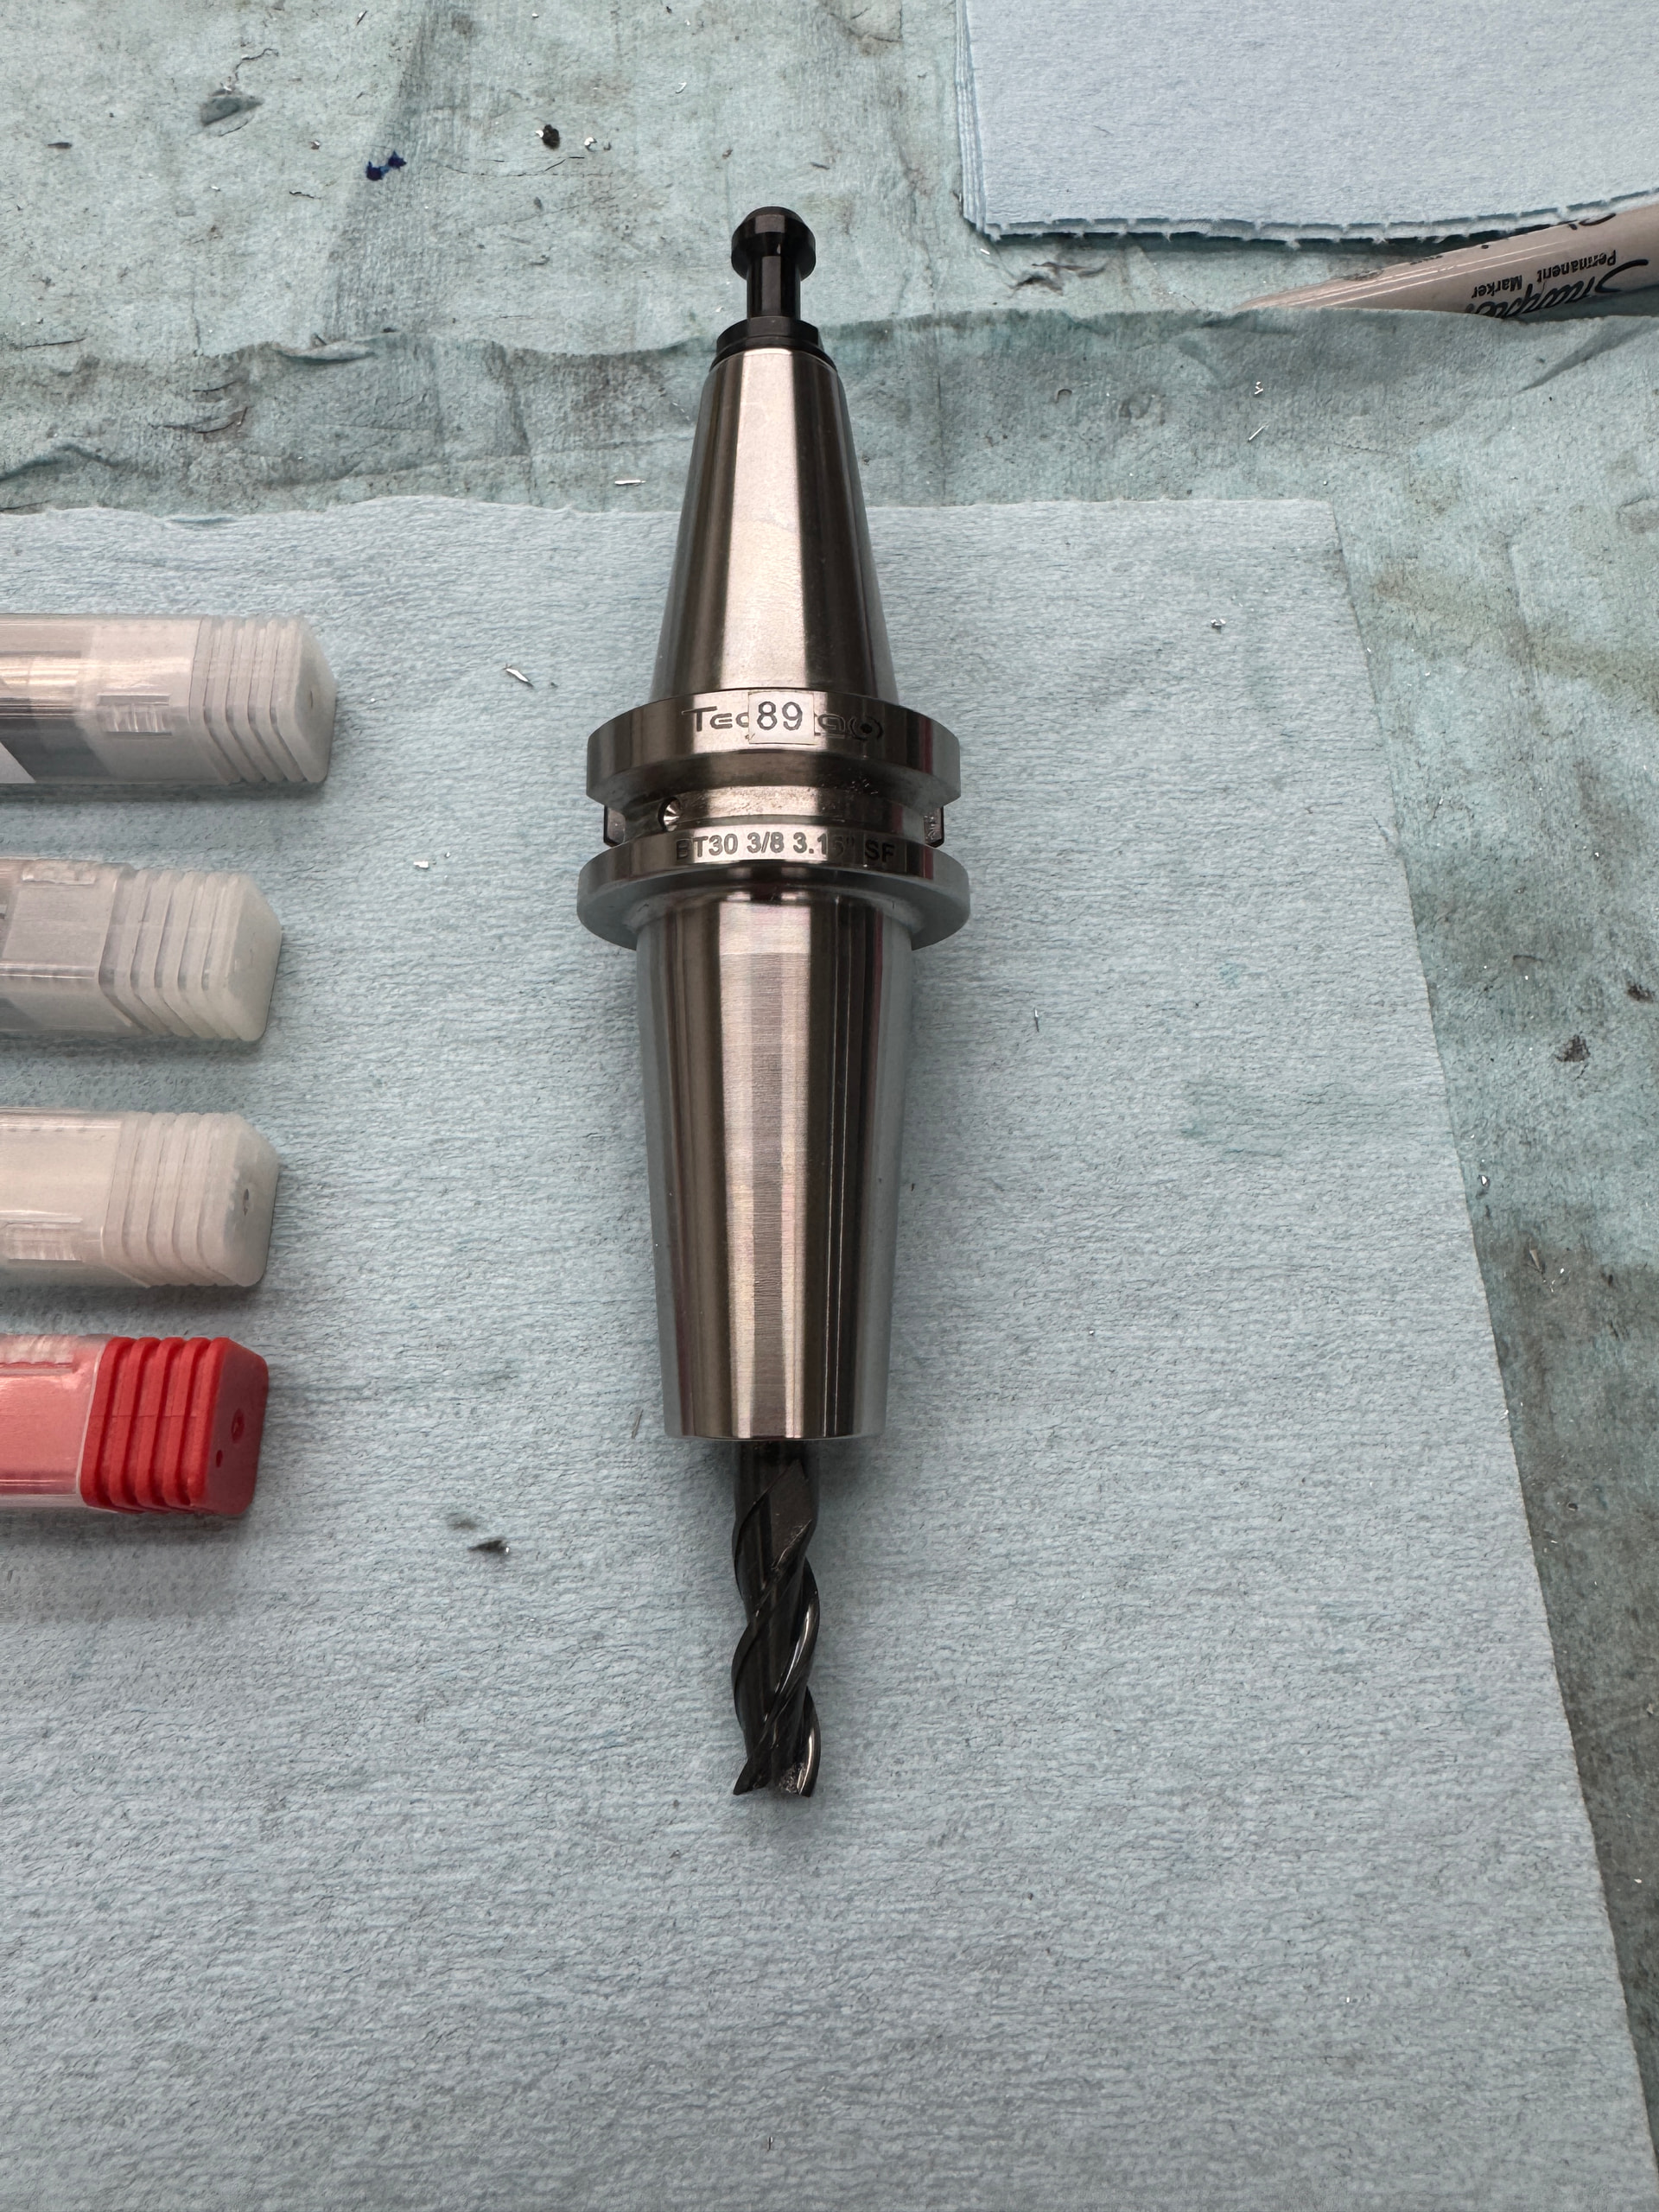
also is a Tegara shink fit in 3/8 I use these on all the finishing EM’s for low TRO and rigidity, they cost about $135 and easy to use a propane torch to install or remove an EM
You might also try a 1/2” EM…. to me a .030 WOC at a 1” or really any DOC is too much for a 3/8” especially a long one…